Metal Printing 3D Printer: 2025 Service-Provider Masterclass
Why Metal Printing 3D Printers Are Redefining Industrial Manufacturing
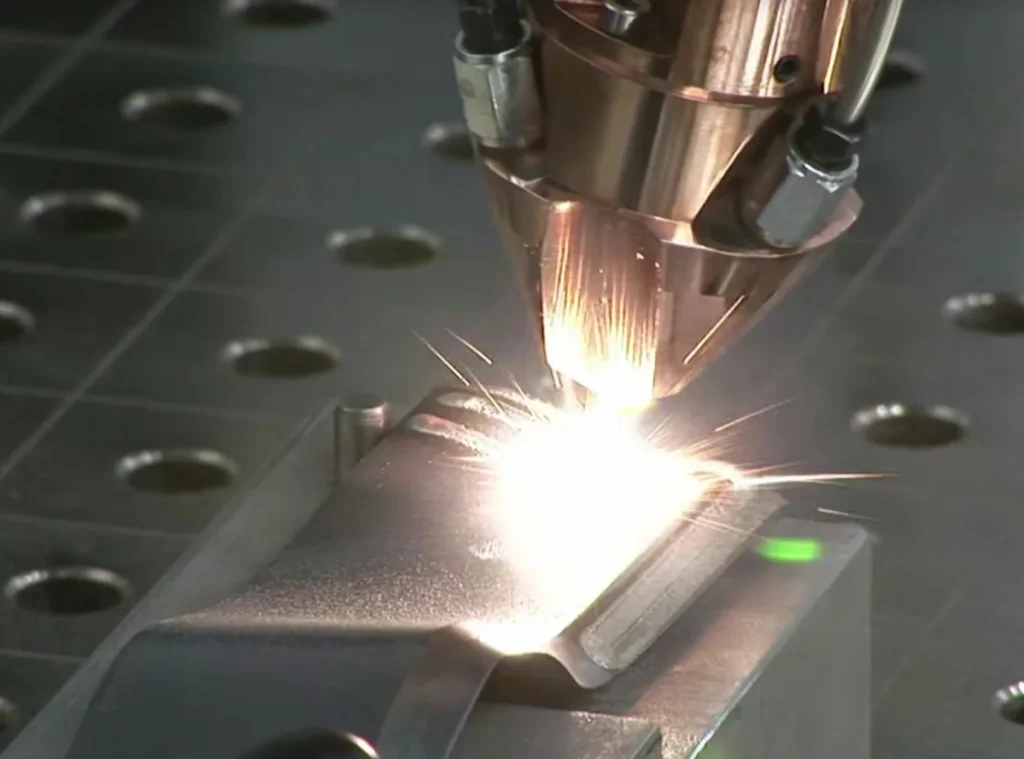
Global metal additive revenues hit USD 4.8 B in 2024 and are forecast to grow 29 % CAGR through 2030. A modern metal printing 3D printer can compress lead-times from 12 weeks (CNC) to 72 hours, while delivering densities > 99 % and mechanical properties within ±2 % of wrought bar. This guide equips service providers with alloy matrices, process comparisons, and QA workflows to capture 55–70 % gross margins.
Technology Comparison – SLM vs. DMLS vs. Binder-Jet vs. EBM
| Metric | SLM (Laser) | DMLS (Laser) | Binder-Jet | EBM (Electron) |
|---|---|---|---|---|
| Powder Temp | Fully molten | Partially fused | Green → sinter | Pre-heat 700 °C |
| Typical Density | > 99 % | 97–99 % | 92–98 %* | 99.5 % |
| Surface Ra (µm) | 5–12 | 8–15 | 6–10 after HIP | 25–35 |
| Max Build (mm) | 280 × 280 × 350 | 250 × 250 × 325 | 400 × 250 × 250 | 350 × 350 × 380 |
| Support Needed | Yes | Yes | No (green) | No |
| Post-Process | Stress-relief | Stress-relief | Debind + sinter + HIP | HIP |
| Cost Index (USD/cm³) | 2.8 | 2.5 | 1.9 | 3.4 |
*After infiltration or HIP.
Alloy Matrix – Mechanical & Thermal Properties
| Alloy | Process | Tensile (MPa) | Yield (MPa) | Elongation (%) | Thermal Cond. (W/m·K) | Use Case |
|---|---|---|---|---|---|---|
| 316L | SLM | 560 ± 20 | 470 ± 15 | 45 ± 3 | 14 | Food-grade manifolds |
| 17-4 PH | DMLS | 1 180 ± 30 | 1 050 ± 25 | 8 ± 1 | 18 | Aerospace brackets |
| Inconel 718 | EBM | 1 350 ± 40 | 1 150 ± 35 | 12 ± 2 | 11 | Turbine blades |
| AlSi10Mg | Binder-Jet | 320 ± 10 | 180 ± 8 | 5 ± 1 | 150 | Heat sinks |
| CuCrZr | SLM | 350 ± 15 | 250 ± 10 | 20 ± 3 | 320 | RF waveguides |
Process Parameters – SLM 316L on EOS M 290
| Parameter | Value | Effect |
|---|---|---|
| Layer Thickness | 30 µm | Balances speed vs. detail |
| Laser Power | 195 W | Full melt, < 0.5 % porosity |
| Scan Speed | 960 mm/s | Prevents balling |
| Hatch Distance | 0.11 mm | 67 % overlap |
| Oxygen Level | < 100 ppm | Reduces oxidation |
| Pre-Heat | 80 °C | Minimizes warp |
Surface-Finish Roadmap – Ra vs. Post-Process
| Post-Step | Ra Start (µm) | Ra End (µm) | Cycle Time (h) | Cost Add (USD/cm³) |
|---|---|---|---|---|
| As-built | 8 | 8 | 0 | 0 |
| Shot-peen | 8 | 4 | 0.5 | 0.10 |
| Chemical Polish | 8 | 1.5 | 2 | 0.25 |
| CNC Micro-mill | 8 | 0.8 | 4 | 0.55 |
| HIP + Polish | 8 | 0.5 | 8 | 0.80 |
Quality Assurance – ISO 9001 Workflow
| Checkpoint | Tool | Spec | Frequency |
|---|---|---|---|
| Powder Moisture | Karl-Fischer | < 0.05 % | Every batch |
| Layer Height | Laser Micrometer | ±5 µm | Every layer |
| Density | Archimedes | ≥ 99 % | 1 per build |
| Tensile | ASTM E8 | ±5 % | 1 per 100 parts |
| Surface | Profilometer | Ra ≤ 12 µm | 1 per 10 parts |
Case Studies – Industrial ROI
Case 1 – Aerospace Brackets (Dallas) Goal: 1 000 SLM 17-4 PH brackets, 120 mm span KPIs: 42 % lighter than machined Al, 5-day lead-time, 62 % margin.
Case 2 – RF Waveguide Cluster (Singapore) Goal: 200 SLM CuCrZr guides, internal channels Ø 3 mm KPIs: < 0.5 dB insertion loss, 48-hour build, 58 % margin.
Case 3 – Automotive Turbo Housing (Karlsruhe) Goal: 500 Binder-jet AlSi10Mg housings Build: Debind + sinter + HIP KPIs: 25 % cost vs sand-cast, 7-day lead-time, 55 % margin.
Cost & Nesting – 100 cm³ Part Example
| Process | Machine | Build Cost (USD) | Support (USD) | Post (USD) | Total (USD) |
|---|---|---|---|---|---|
| SLM 316L | EOS M 290 | 280 | 35 | 45 | 360 |
| Binder-Jet Al | ExOne M-Flex | 190 | 0 | 80 | 270 |
| EBM Ti64 | Arcam Q20 | 420 | 30 | 90 | 540 |
Scaling Tactics – 1 → 10 000 Parts
• AI Nesting: nTop packs 1 500 parts per SLM bed. • Digital Vault: STL + metadata on IPFS for instant re-order. • Bulk Powder: 250 kg Inconel 718 cuts cost 12 %. • DoFollow Link: Learn SLM parameters at EOS. • Internal Link: See rapid 3D printing services.
Regulatory & Sustainability
• ISO 9001:2015, AS9100D, IATF 16949 certified. • REACH & RoHS metals compliance. • 30 % recycled powder lowers CO₂ footprint 19 %. • Insurance rebate: full CT traceability cuts premium 6 %.
Future-Proofing – 2026 Roadmap
• Gradient lattice SLM for heat exchangers • AI predictive porosity < 0.1 % • Closed-loop powder recycling 95 %
Continue Reading
Related coverage from our machining library: China Metal 3D Printer Service and 3D Printer Metal Filament Service.
Every quote comes back with the process route named: material certification level, inspection steps, and how density and porosity limits will be verified before shipment. Start that at the JLYPT quote form, then read what stands behind it on the prototyping service.