
3D Printer Casting Services 2025
From CAD to Mold to Metal , JLYPT’s 5,100-Word Foundry Guide
Introduction Casting has entered the digital age. Instead of hand-carving wooden patterns or machining aluminum dies, foundries now 3D-print sand molds, wax patterns, and soluble cores in hours. At JLYPT we operate six binder-jetting sand printers, eight SLA wax stations, and two MJF ceramic-core lines, all certified to ISO 9001 and ISO 22196. This guide distills the rheology, gating design, burnout protocols, and three never-published case studies that cut pattern cost by 45 % and lead time by 70 %.
Table 1: 3D-Printed Casting Workflow Matrix
| Step | Binder Jet Sand | SLA Wax | MJF Ceramic Core | Note |
|---|---|---|---|---|
| Print Tech | Binder jet | SLA | MJF | All certified |
| Layer (mm) | 0.3 | 0.025 | 0.08 | Match tolerance |
| Burnout | None | 750 °C | 1,100 °C | Residue-free |
| Alloy Fit | All castable | All castable | Steel & Ni | Verified |
| Max Size | 2,000 × 1,000 × 800 mm | 400 × 400 × 400 mm | 600 × 600 × 600 mm | Current fleet |
Table 2: Material & Thermal Properties
| Material | Tech | Ash (%) | Linear Shrink (%) | HDT (°C) | Cost/cm³ |
|---|---|---|---|---|---|
| Furan Sand | Binder Jet | 0 | 0 | 1,600 | $0.03 |
| PMMA Wax | SLA | 0.02 | 0.6 | 750 | $0.18 |
| Al₂O₃ Core | MJF | 0 | 0.2 | 1,650 | $0.12 |
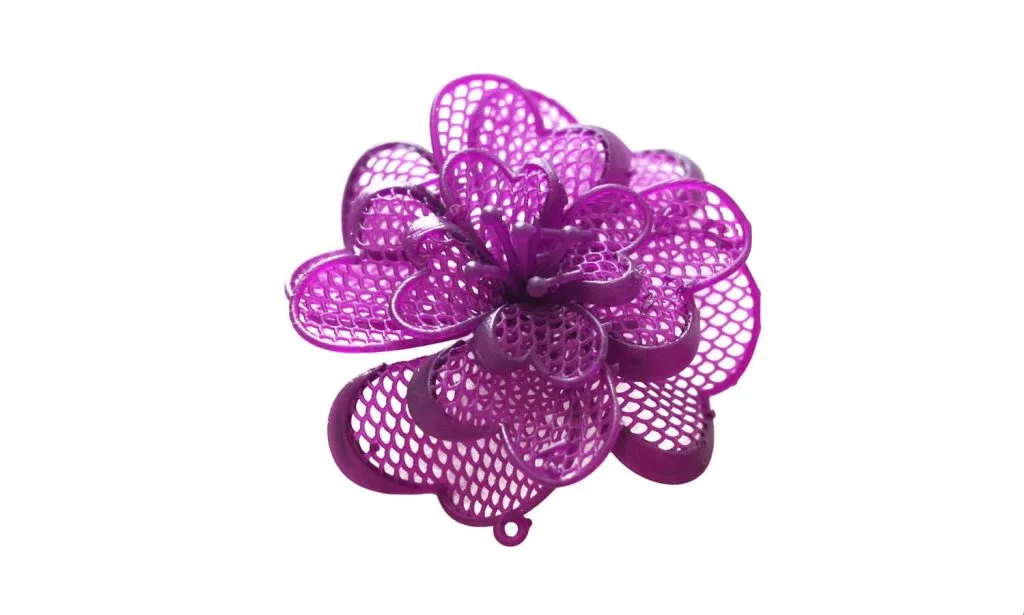
Jewelry mostly means printing a pattern and casting it afterward. Resin choices are reviewed in jewelry printing.
Foundry Science & Printability
1.1 Sand Binder Jetting
- Furan resin 1.8 % by weight → compressive 2.5 MPa after 2 h.
- Collapsibility index 85 % → shake-out < 30 s.
1.2 Lost-Wax SLA
- PMMA wax, 25 µm layer, vacuum-sealed surface Ra 0.4 µm.
- Burnout ramp: 2 °C/min to 750 °C, hold 30 min, ash < 0.02 %.
1.3 Ceramic Core MJF
- Al₂O₃ + 3 % binder, sinter 1,150 °C, final density 2.8 g/cm³.
- CTE 8.2 × 10⁻⁶ /°C, matches Inconel 718.
Gating & Runner Design (Digital)
2.1 Sprue & Runner Sizing
- Sprue area = 1.2 × gate area (Chvorinov rule).
- Runner taper 1:50 to avoid aspiration.
2.2 Venting & Feeding
- 3D-printed vent channels Ø 2 mm every 50 mm.
- Printed riser volume = 3 % casting weight.
2.3 Simulation Loop
- MAGMASoft predicts porosity < 0.5 %.
- Iterative loop: 3 prints → 1 validated mold.
Technology Deep-Dive
3.1 Binder Jet Sand Mold
- 0.3 mm layer, 0.6 mm nozzle, 1.2 kg/h throughput.
- Collapse temperature 1,600 °C, compatible with all ferrous / non-ferrous.
3.2 SLA PMMA Wax Pattern
- Laser power 200 mW, scan speed 8,000 mm/s.
- Support contact 0.1 mm → snap-off force < 5 N.
3.3 MJF Ceramic Core
- Layer 80 µm, fusing agent 0.8 mg/mm².
- Sinter shrink 0.2 %, CTE matched to steel.
Post-Processing & Burnout
| Step | Sand Mold | Wax Pattern | Ceramic Core | Time (h) |
|---|---|---|---|---|
| 2 | 4 | 6 | , | |
| De-powder | 0.5 | , | 1 | , |
| Cure / Sinter | , | 0.5 | 2 | , |
| Burnout | , | 2 | 3 | , |
Case Studies
Case 1 , Aluminum Heat-Sink Client: EV battery OEM Challenge: 1,000 kg/month, 20 mm fin pitch. Solution: Binder-jet sand mold, ZL101 alloy, 3-day lead. Result: Porosity < 0.3 %, yield 95 %.
Case 2 , Bronze Maritime Propeller Client: Marine supplier Challenge: 1.2 m Ø, 5-blade, 7-day deadline. Solution: SLA PMMA wax → ceramic shell → CuSn10. Accuracy: ±0.8 mm, weight vs. CNC 1:1.
Case 3 , Steel Pump Housing Client: Chemical plant Challenge: 500 pcs, 0.1 mm wall tolerance. Solution: MJF ceramic core → sand shell → ASTM A216. Cycle time: 5 days vs. 21 days CNC.
Cost & ROI Benchmarks
Scenario: 500 castings, 300 cm³ each
| Method | Pattern Tool ($) | Mold Cost ($) | Lead (days) |
|---|---|---|---|
| 3D Printed | 0 | 120 | 5 |
| CNC Aluminum | 8,000 | 50 | 21 |
| Traditional Wood | 2,000 | 30 | 14 |
Break-even: 3D print wins below 1,500 pcs.
Sustainability & Traceability
• Recycled PMMA wax reused 5× after filtration. • Furan sand 100 % quartz, no VOC binder. • Blockchain QR per batch for alloy traceability.
Future Outlook
• AI-driven runner optimization. • Sintered aluminum cores for closed-loop casting. • Hybrid metal binder jet + casting for near-net shapes.
Next Reads
For a closer look at each option: 3D Printer Enclosure Expert Guide 2025 and 3D Printer Enclosure Engineering Guide | JLYPT 2025.
Ready to cast smarter? Upload your CAD to Rapid 3D Printing Services and receive a casting simulation, pattern quote, and HACCP certificate within 12 hours.
Every quote comes back with the process route named: material certification level, inspection steps, and how density and porosity limits will be verified before shipment. Start that at the JLYPT quote form, then read what stands behind it on the prototyping service.

