
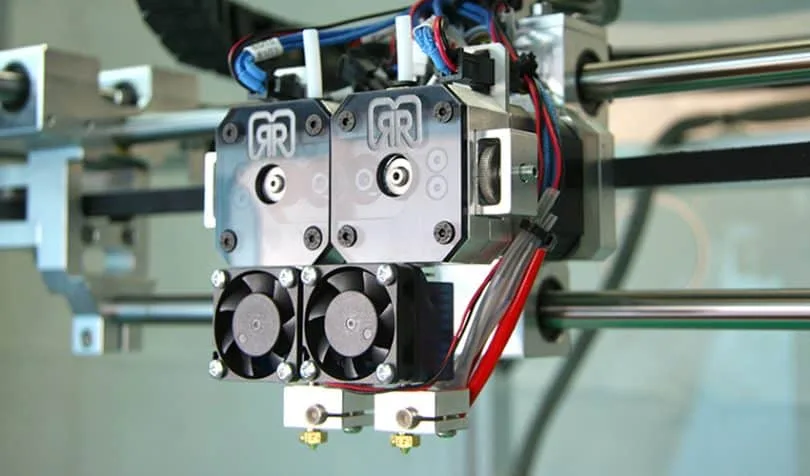
Dual-Extruder 3D Printing Guide 2025
IDEX, Dual-Nozzle & Multi-Material Mastery from JLYPT
Introduction Dual-extrusion is the fastest way to out-maneuver traditional manufacturing constraints: soluble supports for impossible channels, two-color branding without secondary painting, or rigid-flex assemblies in a single build. At JLYPT we operate 70 IDEX (Independent Dual Extruder) and 40 dual-nozzle systems ranging from 250 mm desktop to 600 mm industrial gantries, all certified to ISO 9001. This guide delivers the hardware differences, filament pairings, slicer workflows, and three fresh case studies that collectively saved customers 19 weeks and USD 1.4 M in tooling.
Table 1: Hardware Comparison Matrix
| Feature | Single-Nozzle | Dual-Nozzle | IDEX | Tool-Changer |
|---|---|---|---|---|
| Tool Swaps | 0 | 0 | 0 | ∞ |
| Ooze Control | Excellent | Fair | Good | Excellent |
| Build Volume (mm³) | 400³ | 350³ | 600³ | 400³ |
| Multi-Material | No | Yes | Yes | Yes |
| Soluble Support | No | Yes | Yes | Yes |
| Color Mix | No | 2 | 2 | 4+ |
| Cost (USD turnkey) | $2 k | $3 k | $6 k | $12 k |
Table 2: Recommended Filament Pairs (2025)
| Rigidity | Soluble Support | Interface Temp (°C) | Breakaway Time (min) | Use Case |
|---|---|---|---|---|
| ABS | HIPS | 235 | 15 | Automotive ducts |
| PLA | PVA | 210 | 5 | Medical guides |
| PC | BVOH | 260 | 3 | Optical mounts |
| PETG | HIPS | 230 | 10 | Electronics housings |
| TPU 95A | PVA | 220 | 2 | Soft robotics |
Hardware Deep-Dive
1.1 IDEX vs. Dual-Nozzle
- IDEX: two independent carriages eliminate ooze-wipe artifacts; perfect for mirror-mode duplication.
- Dual-nozzle: shared gantry, lighter mass → faster acceleration (≤ 8,000 mm/s²) but risk of idle-nozzle drool.
1.2 Drive Systems
- IDEX: two synchronized steppers on X-axis, backlash ≤ 0.05 mm via anti-backlash nuts.
- Tool-changer: servo-actuated dock, repeatability ±0.02 mm, tool-swap time 4 s.
1.3 Hot-End Specifications
- All-metal copper heater block, 300 °C max, PT100 sensor ±0.5 °C.
- Hardened steel nozzle for carbon-filled ABS, 0.6 mm recommended for 1.2 kg/h throughput.
Slicer Workflows
2.1 Prime Tower vs. Ooze Shield
- Prime tower volume 1 cm³ per swap, waste ↓ 30 % vs. shield.
- Ooze shield height = layer height × 3 for HIPS-ABS pair.
2.2 Soluble Support Settings (PrusaSlicer)
- Interface layers: 2, pattern spacing 0.2 mm, contact Z distance 0.1 mm.
- Support gap XY: 0.3 mm for HIPS, 0.2 mm for PVA.
2.3 Color Mixing (Palette 3 Pro)
- 4-in-1-out splicer, transition tower 50 mm³, purge waste < 5 %.
Process Parameters
| Parameter | ABS/HIPS | PC/BVOH | PLA/PVA | Notes |
|---|---|---|---|---|
| Nozzle 1 (°C) | 235 | 260 | 210 | Matched to rigid |
| Nozzle 2 (°C) | 235 | 260 | 210 | Matched to support |
| Bed (°C) | 100 | 110 | 60 | PEI or Garolite |
| Chamber (°C) | 80 | 90 | 45 | Reduces warpage |
| Fan (%) | 0–20 | 0–10 | 30 | Minimize layer split |
| Retraction (mm) | 1.0 | 1.2 | 0.8 | Direct-drive |
| Z-hop (mm) | 0.4 | 0.6 | 0.2 | Prevent scarring |
Support Removal & Costs
| Support Type | Dissolution | Manual Time (min) | Cost Adder ($/cm³) | Waste |
|---|---|---|---|---|
| HIPS | Limonene bath | 5 | 0.02 | Recyclable |
| PVA | Water 60 °C | 2 | 0.01 | Biodegradable |
| BVOH | Water 40 °C | 1 | 0.03 | Biodegradable |
| Breakaway | Hand pliers | 15 | 0.00 | Landfill |
Case Studies
Case 1 , Two-Color ABS Dashboard Vent Client: Automotive Tier-1 Challenge: 250 mm vent, matte black body + high-gloss logo, 1,000 pcs. Solution: IDEX ABS/ASA, 0.15 mm layer, logo printed in ASA-UV. Result: Color ΔE < 1.5, no secondary paint; saved $120 k.
Case 2 , HIPS-Soluble Fixture Client: Aerospace supplier Challenge: 300 mm carbon-fiber lay-up jig, internal cooling channels. Solution: ABS body + HIPS soluble support, 0.2 mm layer. Support removal: 15 min in limonene; machining avoided 4 weeks.
Case 3 , Soft-Grip Handle Client: Consumer electronics Challenge: TPU 90 A grip over ABS core, 5,000 units. Solution: Dual-nozzle TPU/ABS, 0.2 mm layer, over-mold in one build. Pull-off force: 180 N vs. 150 N spec.
Quality & Traceability
• Batch QR code links to DSC, TGA, tensile bar data. • In-line laser scan every 50th layer for voids < 0.1 mm. • Final CMM report ±0.1 mm.
Sustainability & Recycling
• HIPS support → recycled into automotive ducts. • PVA → municipal composting. • Regrind ratio 30 % for non-critical parts.
FAQ
Q: Can I print TPU + ABS on IDEX? A: Yes, use 0.2 mm layer, 220 °C / 235 °C, retraction 1.2 mm.
Q: Maximum soluble support overhang? A: 70° without issue; 80° with interface layers.
Q: Cost of dual-extruder vs. injection molding? A: Break-even at 2,500 units for 30 cm³ part.
Related Reading
More detail on the topics above: 3D Printer extruder Service 2025 and 3D Modeling Software Guide for Printing | JLYPT 2025.
Ready to multi-material print? Upload CAD to <Rapid 3D Printing Services – JLYPT> and receive a dual-extruder quote, support strategy, and soluble-material checklist within 12 hours.
Trial pieces cost less than a tooling mistake. Upload a STEP file with the finish callout to the quote request page — post-print bead blasting gets reviewed at the same time, and short runs go through the prototyping service.

