
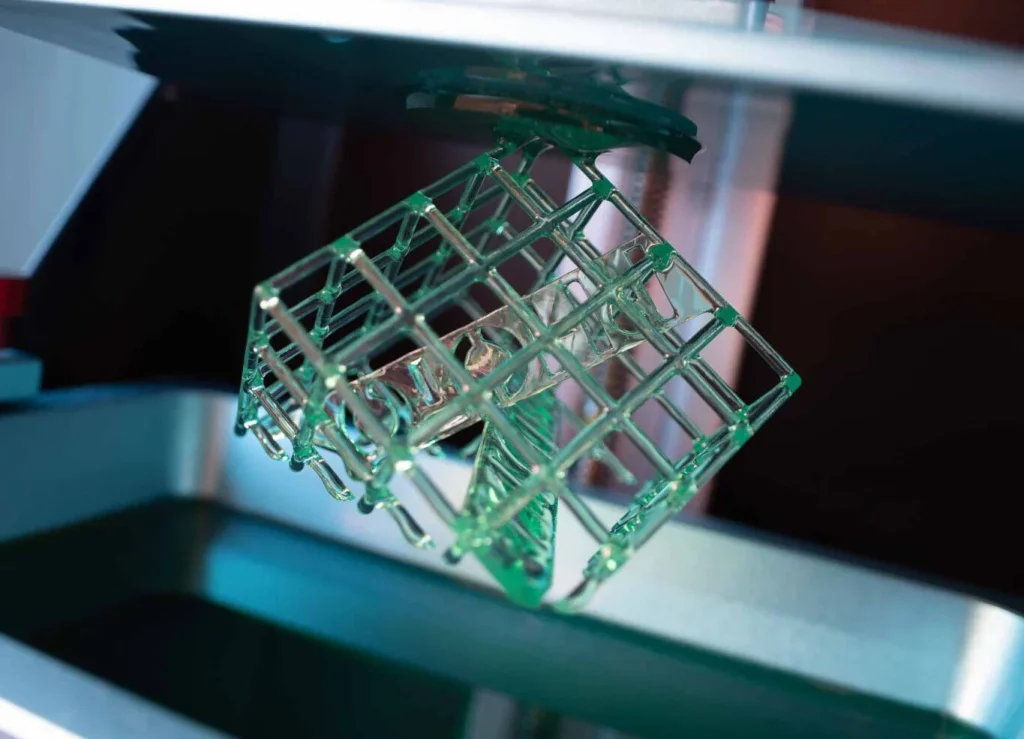
Precision SLA 3D Printing Services
A 2025 Guide for Engineers, Dentists & Designers
Introduction Stereolithography (SLA) remains the gold standard when surface finish, fine features, and tight tolerances matter. By curing liquid photopolymer with a UV laser, SLA delivers injection-mold quality without molds, ideal for prototypes, master patterns, and low-volume end-use parts. JLYPT operates 60 industrial SLA systems, including eight Formlabs Form 3L and two Nexa3D NXE 400Pro units, capable of 25 µm Z resolution and 350 × 350 × 400 mm builds. This guide distills resin science, design tactics, cost levers, and three fresh case studies that saved clients weeks and tens of thousands in tooling.
Table 1: SLA Resin Portfolio (2025)
| Resin | Tensile (MPa) | Flex Mod (MPa) | HDT (°C) | Use Case | Color |
|---|---|---|---|---|---|
| GP-Clear 25 | 65 | 2,300 | 52 | Optics, lenses | Water-clear |
| Tough-X | 80 | 2,800 | 60 | Snap-fits | White |
| Dental Model | 75 | 2,600 | 65 | Ortho models | Beige |
| Castable Purple | 45 | 2,100 | 45 | Jewelry wax | Purple |
| Bio-Med Clear | 55 | 2,200 | 50 | Surgical guides | Translucent |
| High-Temp Gray | 95 | 3,400 | 120 | Under-hood | Gray |
| ESD-Safe | 50 | 2,300 | 55 | Electronics | Black |
Table 2: Layer Height vs. Surface & Time
| Layer (µm) | XY (µm) | Surface Ra (µm) | Build Speed (mm/h) | Relative Cost | Best For |
|---|---|---|---|---|---|
| 25 | 75 | 0.8 | 12 | 3.0× | Micro-fluidics |
| 50 | 75 | 1.2 | 25 | 1.8× | Dental models |
| 100 | 75 | 2.0 | 45 | 1.0× | Prototypes |
| 200 | 75 | 3.5 | 80 | 0.7× | Draft housings |
Design Guidelines for SLA Success
1.1 Wall & Feature Size
- Minimum wall: 0.4 mm for GP resins, 0.6 mm for filled grades.
- Pins & text: 0.35 mm positive height, 0.5 mm width to prevent wash-away.
1.2 Drain & Vent Holes
- Hollow parts ≥ 2 mm drain every 30 mm cavity length.
- Angled 45° to avoid resin pooling.
1.3 Support Strategy
- Light-touch supports (tip Ø 0.3 mm) leave <0.1 mm nibs.
- Use internal supports on cosmetic faces to keep exterior flawless.
1.4 Tolerance Budget
- Standard: ±0.1 mm or ±0.1 %, whichever larger.
- Post-cure shrinkage: compensate +0.05 % on critical fits.
Post-Processing Roadmap
| Step | Equipment | Time | Notes |
|---|---|---|---|
| Ultrasonic wash | 99 % IPA bath | 5 min | Removes uncured resin |
| UV cure chamber | 405 nm, 60 °C | 15 min | Nitrogen purge for tack-free finish |
| Support removal | Micro-shears | 2–5 min | Leaves <0.1 mm nibs |
| Light polish | 3,000 grit | 5 min | Boosts clarity for clear resins |
| UV coating | Spray booth | 10 min | Scratch resistance for lenses |
Cost Drivers & Instant Estimator
| Factor | Impact | Tip to Save |
|---|---|---|
| Volume | Linear | Hollow + lattice |
| Height | Exponential | Orient flat |
| Layer | 2× cost @ 25 µm | Use 50 µm for drafts |
| Resin | GP vs. specialty | Validate fit with GP first |
| Finish | Polish adds 30 % | Limit to visible faces |
Instant Quote Table (50 µm layer)
| Volume Range | Standard Resin | Specialty Resin | Rush (24 h) |
|---|---|---|---|
| < 50 cm³ | $0.18 / cm³ | $0.25 / cm³ | +100 % |
| 50–200 cm³ | $0.14 / cm³ | $0.20 / cm³ | +100 % |
| 200–1,000 cm³ | $0.11 / cm³ | $0.16 / cm³ | +100 % |
| > 1,000 cm³ | Custom | Custom | Custom |
Case Studies
Case 1 , High-Resolution Camera Lens Barrel Client: Smartphone OEM Challenge: 14 mm Ø lens barrel, ±25 µm concentricity, clear optical path. Workflow:
-
Designed in SolidWorks, split into four threaded sections.
-
Printed in GP-Clear 25 µm layers.
-
CNC-turned M9 × 0.5 threads post-print.
-
Light-transmission test: 92 % @ 550 nm.
Lead time: 5 days vs. 6-week diamond-turned PMMA.
Case 2 , Custom Dental Surgical Guide Client: Oral surgery clinic Challenge: 8-implant guide, biocompatible, fit within 0.05 mm. Solution:
-
CBCT DICOM → Meshmixer → Onshape for sleeve bosses.
-
Printed in Bio-Med Clear, 50 µm.
-
Sterilized via autoclave 134 °C, 30 min.
Outcome: Reduced chair time by 35 %, zero re-prints.
Case 3 , Luxury Jewelry Master Pattern Client: Milan atelier Challenge: 18 k gold ring, filigree 0.3 mm, 30-piece limited run. Workflow:
-
Blender sculpt + ZBrush detailing.
-
Printed in Castable Purple, 25 µm.
-
Lost-wax cast in 18 k gold.
-
Surface Ra 0.4 µm straight from mold, no hand engraving.
Revenue: Sold out at €1,200 each.
Choosing Between SLA, DLP & FDM
| Scenario | SLA | DLP | FDM |
|---|---|---|---|
| < 0.3 mm features | ✓ | ✓ | ✗ |
| Transparent optics | ✓ | ○ | ✗ |
| 10+ cm³ volumes | Costly | Costly | Cheap |
| High-temp (>120 °C) | Limited | Limited | ✓ |
| ESD-safe | ✓ | ✓ | ✓ |
Sustainability & Bio-Resins
• Plant-based Bio-Med Clear reduces CO₂ by 35 %. • IPA distillation unit recovers 94 % solvent. • Failed prints cured into desk organizers, zero landfill.
FAQ
Q: Can SLA parts be tapped? A: Yes, print undersized by 0.1 mm and chase with tap; use Tough-X for durability.
Q: Maximum clear part thickness? A: 5 mm before light scattering; above 5 mm use hollow with 1 mm walls.
Q: Will clear resin yellow outdoors? A: Add UV-block topcoat or switch to High-Temp Gray for outdoor use.
Next Reads
For a closer look at each option: High-Resolution Resin 3D Printing Services and 3D Printing vs CNC Machining.
Ready to quote? Drag your STL into <url id=”d268lcnf2en4q1cioc4g”> and receive a live price, orientation preview, and free DFM report in minutes.
A finished sample settles arguments about as-printed versus machined tolerance faster than a spec sheet does. Ask for one through the JLYPT quote page; the prototyping service shows what the surface looks like off the line.

